
New Standards for Cleanroom Grades and Environmental Requirements in Advanced Packaging
Advanced packaging has changed the rules of semiconductor manufacturing, and cleanroom standards are changing with it. What used to be a largely front-end concern is now a packaging concern too, because heterogeneous integration depends on much more than just transistor quality. It depends on the cleanliness of bonding surfaces, the stability of thin wafers, the behavior of mold compounds, the integrity of fine-pitch interconnects, and the control of particles, humidity, and temperature throughout assembly. In short, the environment has become part of the design.
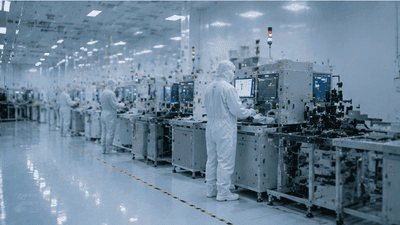
That is why new standards for cleanroom grades and environmental requirements in advanced packaging are so important. As packages become more complex and more sensitive, the factory environment must become more disciplined. A particle that would have been minor in an older package can now ruin a hybrid bond. A small humidity variation can affect underfill, molding, or adhesion. A tiny amount of airborne contamination can undermine the yield of an entire 2.5D or 3D stack. The result is a packaging industry that increasingly treats environmental control not as a support function but as a core manufacturing capability.
Why Advanced Packaging Needs Stricter Environments
The move toward advanced packaging and heterogeneous integration has made packages much more delicate. A modern package may contain several dies, an interposer, high-bandwidth memory stacks, redistribution layers, fine-pitch bumps, or even direct-bonded 3D structures. These technologies demand extremely tight process windows. The more sensitive the geometry, the less tolerance there is for contamination, warpage, or moisture-related defects.
In older packaging, a small particle might not be fatal because interconnect pitch was wider and the package structure was more forgiving. In advanced packaging, that same particle can prevent proper bonding or create a localized defect that affects yield and long-term reliability. Likewise, environmental drift that once might have been acceptable can now change alignment, surface chemistry, or material behavior enough to matter. That is why cleanroom grades and environmental requirements are tightening across the advanced packaging chain.
The shift is not just technical. It is also economic. Advanced packaging is now part of the value creation process for AI, HPC, mobile, automotive, and networking systems. If the environment causes defects, the cost per functional package rises quickly. Better environmental control is not just about quality; it is about protecting the economics of the entire manufacturing flow.
From Front-End Thinking to Back-End Precision
Traditionally, the strictest cleanroom standards were associated with front-end wafer fabrication. Packaging, assembly, and test often operated under less demanding environmental assumptions. That separation is no longer viable. As fan-out, wafer-level packaging, hybrid bonding, and 3D integration move into volume manufacturing, many packaging steps now require front-end-like cleanliness and tighter environmental discipline.
This is especially true for:
- Hybrid bonding, where surface contamination can directly prevent bonding.
- Fine-pitch flip-chip and micro-bump assembly, where alignment and particle control are critical.
- Fan-out wafer-level and panel-level packaging, where redistribution layer integrity depends on clean surfaces.
- 3D stacking, where thin wafers and complex interfaces are especially sensitive to environment-driven defects.
The key change is philosophical. Packaging is no longer “downstream” in the sense of being less demanding. It is downstream in sequence, but not in sophistication. In many advanced packaging flows, the environmental burden is now every bit as serious as it is in a fab.
What Cleanroom Grades Are Really About
Cleanroom grades define how many particles are allowed in a given volume of air, along with related parameters such as airflow, filtration, temperature stability, and relative humidity. In advanced packaging, the exact grade required depends on the process step. A molding operation may not need the same level of cleanliness as a hybrid bonding surface preparation area, but both need tighter control than older legacy packaging lines.
The most important point is that one cleanroom grade does not fit every advanced packaging process. Different operations have different sensitivity:
- Bonding and surface activation require the cleanest environments because even tiny particles can block contact.
- Wafer thinning and temporary bonding need low contamination and tight humidity control to protect fragile wafers.
- Fan-out molding and redistribution need clean, stable conditions to avoid defects in fine features.
- Final assembly and test still require controlled environments, though the exact grade can vary depending on package type.
New standards are increasingly moving toward process-specific environmental definitions instead of relying only on broad generic cleanroom labels. That is a healthy shift because advanced packaging is no longer one process. It is a family of processes with different sensitivities and failure modes.
Particles Are Still the Enemy
If there is one universal enemy in advanced packaging, it is the particle. A speck of contamination may be nearly invisible to the human eye, but in a fine-pitch package it can be catastrophic. It may cause a void, an open interconnect, a weak bond, or a latent reliability issue that only appears after thermal cycling. In hybrid bonding, the risk is especially acute because the interface is direct and extremely fine.
That is why new environmental requirements place such a strong emphasis on airborne particle control, surface cleanliness, and material handling discipline. It is not enough to have clean air in the room. The entire flow must be designed to minimize contamination during transfer, storage, staging, and bonding. This includes the behavior of carriers, trays, tools, handling systems, and even operators.
Advanced packaging lines now need to think about contamination in layers:
- Ambient room particle levels.
- Tool-level cleanliness.
- Surface condition of wafers, dies, and carriers.
- Transfer and staging contamination between steps.
A line can have an excellent cleanroom on paper and still suffer contamination if the process flow is poorly designed. That is why environmental standards increasingly include handling protocols and process integration, not just air filtration.
Humidity and Temperature Matter More Than Ever
Particles are the obvious problem, but humidity and temperature may be just as important. Many advanced packaging materials are sensitive to moisture absorption, curing behavior, and thermal expansion. A slight change in humidity can affect mold compounds, adhesives, underfills, and surface chemistry. A small temperature drift can influence alignment, warpage, and bond quality.
This matters because advanced packaging often uses thin wafers, large substrates, and multi-material stacks. Those structures respond strongly to environmental changes. If the room is too humid, materials can absorb moisture and change behavior. If the temperature is unstable, the package may warp or lose precise registration. In extreme cases, these effects can ruin yield long before the package reaches final qualification.
New standards therefore push for tighter control of relative humidity and temperature, especially in high-sensitivity areas like bonding, die attach, and hybrid integration. The more advanced the package, the more the environment must behave like a process tool rather than a background condition.
Advanced Packaging Needs Zoning
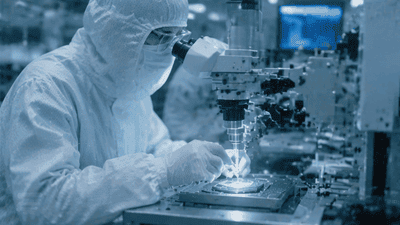
One of the most practical ideas in new environmental standards is zoning. Not every step in a packaging flow needs the same cleanroom grade, but the most sensitive steps should be isolated in dedicated environments. This allows manufacturers to apply stricter control where it matters most without turning every square foot of the facility into the most expensive possible cleanroom.
For example, a packaging line might include:
- A high-grade bonding zone for hybrid bonding or fine-pitch die placement.
- A controlled thinning and temporary bonding zone for wafer preparation.
- A more moderate assembly or molding zone for less sensitive steps.
- A separate test and inspection zone with stable environmental conditions.
This approach is efficient and realistic. It recognizes that advanced packaging is a chain of different activities, each with its own environmental sensitivity. Zoning also helps reduce cross-contamination by limiting the movement of particles, moisture, and materials between process areas.
Why Heterogeneous Integration Raises the Bar
Heterogeneous integration complicates the environment because it combines different materials, dies, and process flows in one system. Silicon, glass, organic substrates, mold compounds, adhesives, thermal interfaces, and metal structures all behave differently. When these materials are brought together in a package, environmental control becomes essential to prevent unwanted interactions.
A package that includes multiple dies from different process nodes may also include different thermal and mechanical behaviors. Some dies are thin and fragile. Others are power-dense and heat-sensitive. Some interfaces demand perfect planarization. Others require moisture-resistant handling. The environmental requirements rise because the package is no longer designed around one dominant material. It is designed around coexistence.
That is why advanced packaging standards increasingly need to account for system-level material behavior. Cleanroom grade alone is not enough. The standards also need to consider surface preparation, storage conditions, transfer windows, and the sequence of environmental exposures throughout the packaging process.
New Standards Are Becoming More Process-Specific
The industry is gradually moving away from one-size-fits-all cleanliness labels and toward process-specific environmental rules. That is a sensible move. A fan-out redistribution process has different risks than a 3D bonding step. A wafer-level molding process has different contamination sensitivity than a post-bond inspection operation. Standards that reflect those differences are more useful than broad, generic categories.
This trend also helps companies compare requirements more realistically. Instead of asking whether a facility is “clean enough,” engineers can ask whether a specific process window is controlled enough for the package they are building. That is a much better question. It encourages design teams, process engineers, and materials suppliers to think about the environment as part of the packaging recipe rather than as an abstract background constraint.
It also makes qualification more meaningful. If a process is validated under a specific humidity range, temperature range, and contamination budget, then the production line can be managed against those exact conditions. That reduces guesswork and improves reproducibility.
Operational Discipline Becomes Part of the Standard
Environmental control in advanced packaging is not only about building a better room. It is also about operational discipline. The best cleanroom in the world cannot compensate for sloppy transfer, poor storage, or inconsistent tool maintenance. That is why new environmental expectations extend beyond facility design and into manufacturing behavior.
The most successful advanced packaging operations pay attention to:
- How wafers and dies are stored between steps.
- How long sensitive surfaces remain exposed before bonding.
- How carriers and trays are cleaned and qualified.
- How tool uptime and particle generation are monitored.
- How operator movement is managed across zones.
In other words, environmental quality is a system property. It is created by people, tools, materials, and flow design, not just by a room specification. That is especially true in advanced packaging, where the package itself is so sensitive that a brief lapse can create a defect with very expensive consequences.
Test and Inspection Need Cleaner Assumptions Too
Even inspection and test are affected by the rise in environmental standards. Some packages may be clean when assembled but become vulnerable if handled too roughly or exposed too long before test. Others may require environmental stability during metrology to ensure accurate readings. As packages become more heterogeneous, the link between environment and test quality becomes stronger.
That means the new standards are not only about preventing defects during assembly. They are also about preserving the integrity of the data used to judge quality. If the environmental conditions drift, inspection results become less reliable. In a high-value advanced packaging flow, that is a serious problem because a false pass or false fail can cost time, money, and confidence.
The Business Case for Tighter Standards
Stricter environmental control sounds expensive, and it is. Better cleanrooms, tighter humidity regulation, better filtration, and stricter handling all add cost. But in advanced packaging, the cost of poor control is often much higher. A bad bond, a warped package, or a contaminated interface can scrap a high-value module worth far more than the extra environmental overhead.
That is why companies are increasingly viewing cleanroom upgrades as investments rather than overhead. Better environmental standards can:
- Improve yield.
- Reduce rework and scrap.
- Support more complex package architectures.
- Increase process repeatability.
- Strengthen customer confidence in reliability.
When packaging becomes a differentiator for AI, HPC, automotive, and chiplet platforms, yield is worth money, and environmental control becomes a lever for protecting that yield.
Looking Ahead
As advanced packaging continues to evolve, environmental standards will likely become even more specialized. Hybrid bonding may require ultra-clean micro-environments. Panel-level packaging may demand tighter control over large-format handling and warpage. 3D stacking may require zone-specific humidity and temperature rules. The factory of the future may look less like one giant cleanroom and more like a carefully segmented ecosystem of controlled environments.
We may also see stronger integration between environmental monitoring and process data. Sensors could track particulate levels, humidity, and temperature in real time and feed that information into yield analytics. That would make environmental control more proactive and less reactive. Instead of waiting for defects to appear, manufacturers could detect and correct conditions before they harm the process.
Conclusion
New standards for cleanroom grades and environmental requirements in advanced packaging reflect a simple but important truth: as packages get more complex, the environment around them matters more. Heterogeneous integration depends on fine features, delicate materials, and tight process windows that cannot tolerate old assumptions about cleanliness and stability.
The future of advanced packaging will belong to the companies that treat the factory environment as part of the package design. That means tighter cleanroom grades where needed, better humidity and temperature control, smarter zoning, and stronger operational discipline. In the world of advanced encapsulation, the environment is no longer just the place where packaging happens. It is one of the reasons packaging succeeds or fails in the first place.
You May Like

Narrowing Spread Between NAND Spot and Contract Prices in 2026 – A Signal
By 2026, one of the most watched metrics in the NAND flash market has started to shift in a subtle but meaningful way: the spread between spot prices and long‑term contract prices is narrowing. For casual observers, this may look like just another incremental change in a notoriously volatile industry. For memory makers, module houses, device OEMs, and data center buyers, however, a tightening gap between spot and contract prices is a signal—a reflection of evolving supply–demand balance, risk perceptions, and strategic behavior on both sides of the market.

Price Divergence Trading Strategies Between NAND Flash and DRAM ETFs
NAND flash and DRAM sit at the core of AI storage and computing power. Both are memory, but they are not the same business. DRAM is main memory—fast, volatile, and central to high‑bandwidth workloads like AI training and inference. NAND is non‑volatile storage—slower than DRAM, but crucial to persistent data and large‑scale object storage. The cycles that drive their pricing and margins overlap, yet they often diverge. That divergence is where trading strategies between NAND and DRAM ETFs become interesting.

China’s HBM Localization Progress: The Catch-Up Pace of CXMT and XMC
China’s drive to localize advanced memory technologies has accelerated over the past several years. High-Bandwidth Memory (HBM) sits near the center of that strategy because it is integral to AI accelerators, high-performance computing (HPC) and other strategic compute platforms. Two domestic players—ChangXin Memory Technologies (CXMT) and XMC (Xianghui Memory, commonly referred to as XMC)—have become focal points in assessing how quickly China can close the gap with international incumbents on HBM die, stacking, and packaging.

Thermal Simulation Challenges and Solutions in 3DIC AI Chip Design
As AI workloads push chips to deliver ever higher compute density, designers are increasingly turning to three‑dimensional integration (3DIC) to stack dies vertically and pack more functionality into limited footprints. While 3DIC architectures unlock significant performance and bandwidth advantages, they also introduce complex thermal behaviors that are far harder to predict and manage than in traditional 2D layouts.

An Attempt at Compiling a Memory+Compute Fusion Thematic Index – A Dual-Track Framework
Most AI investors talk about “compute” as if it were the whole story: GPUs, accelerators, chips, cores. But every one of those cores needs somewhere to read from and write to. Memory and storage define how wide the data highway really is. In practice, AI performance is a fusion of compute and memory, not a solo act. So why do so many indices and ETFs separate them into different silos—one for semiconductors, one for memory, one for data centers—when the actual workloads keep blending them?

Surging Demand for Laser Drilling and Plasma Dicing Equipment in Advanced Packaging
Advanced packaging has become one of the semiconductor industry’s most important growth engines, and it is now pulling a surprising set of process tools into the spotlight. Among the most in-demand are laser drilling and plasma dicing equipment. These machines sit close to the heart of heterogeneous integration, fan-out packaging, wafer thinning, TSV formation, glass substrate processing, and other advanced flows where precision, yield, and throughput matter enormously. As packaging moves from a back-end afterthought to a strategic platform, the equipment used to shape, open, and separate materials has become just as important as the dies themselves.

D2D Interface Bandwidth and Latency Comparison in Chiplet Architectures
Chiplet architecture has turned the package into a real performance battleground. Once multiple dies are placed side by side or stacked within the same advanced package, the quality of the die-to-die, or D2D, interface becomes one of the most important determinants of system behavior. Bandwidth is no longer a nice-to-have metric, and latency is no longer a small implementation detail. Together, they shape whether a chiplet system feels nearly monolithic or frustratingly fragmented.

Stock Selection Logic and Alpha Validation of ESG-Themed Semi ETFs
Semiconductor themed ETFs are no longer just about growth and cycles. A growing subset now layers environmental, social, and governance (ESG) criteria on top of traditional sector exposure. These ESG semi ETFs promise two things at once: access to one of the market’s most powerful secular themes, and alignment with sustainability and governance standards. The pitch is appealing, but it raises two hard questions. First, how exactly are these stocks being selected? Second, does the ESG overlay help, hurt, or leave alpha unchanged?